- Home
- Blog
- Products & solutions
- How does Miraplast achieve consistent part quality in multi-cavity injection molding, and why is the non-return valve crucial?
How does Miraplast achieve consistent part quality in multi-cavity injection molding, and why is the non-return valve crucial?
In a pilot production trial with iQ weight control plus, Miraplast achieved fewer burnermarks, better quality in injection-molded parts, and significantly more reliable closing of the non-return valve. The result: production-quality parts after the second parameter iteration.

-
digital solutions
-
technical molding
Miraplast Kunststoffverarbeitung GmbH—a company established over 60 years ago with locations in Würmla (Austria) and Hungary—is one of the first companies worldwide to implement the latest product in the ENGEL inject AI portfolio in live production: iQ weight control plus.
The first use of iQ weight control plus on an ENGEL victory 80 demonstrated exactly what production professionals strive for:
significantly simplified sample testing
improved and reproducible injection-molded part quality
optimal balancing for multi-cavity molds
efficient injection molding production despite a shortage of skilled workers
The results, expressed in numbers, surprised even experienced set-up technicians:
Production-quality parts as early as the second parameter iteration – Simplified trial runs using only two injection molding process parameters, even without specialized personnel
–10% reduction in energy consumption per cycle – achieved through pressure-optimized and material-friendly process control
50% reduction in the decompression stroke during the injection molding process—thanks to a non-return valve that closes reliably and reproducibly
Why is maintaining consistent part quality in injection molding with multi-cavity molds so challenging?
Consistently high injection-molded part quality is crucial for the production of pipe clamp components using a 4-cavity mold. At the same time, process variations and the closing behavior of the non-return valve make it difficult to achieve reproducible injection molding production.
Typical challenges in day-to-day production:
Surface defects and venting problems at corners and ribs
Time-consuming sample inspection requiring significant skilled labor
Gradual process fluctuations caused by temperature changes, batch changes, or masterbatch addition lead to process instability
Unreliable closure of the non-return valve compromises the reproducibility of injection-molded part quality
The key question was: How can process fluctuations be minimized, the closing behavior of the non-return valve stabilized, and component quality ensured—all without increasing setup time?
Miraplast Kunststoffverarbeitung GmbH employs approximately 80 people at its main location in Würmla and operates 23 injection molding machines, including 17 ENGEL machines. With a deliberately diversified product portfolio, the company cushions the impact of market fluctuations, such as those in the automotive sector.
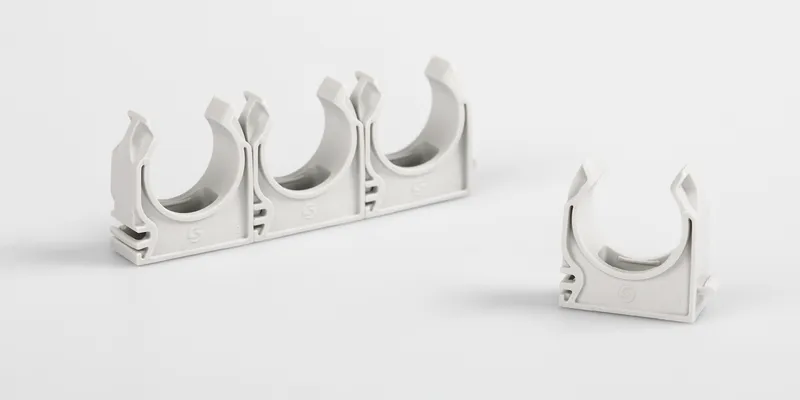
Pipe clamp components manufactured using a 4-cavity mold on an ENGEL victory 80
How was Miraplast able to stabilize part quality in injection molding, and what role does the non-return valve play?
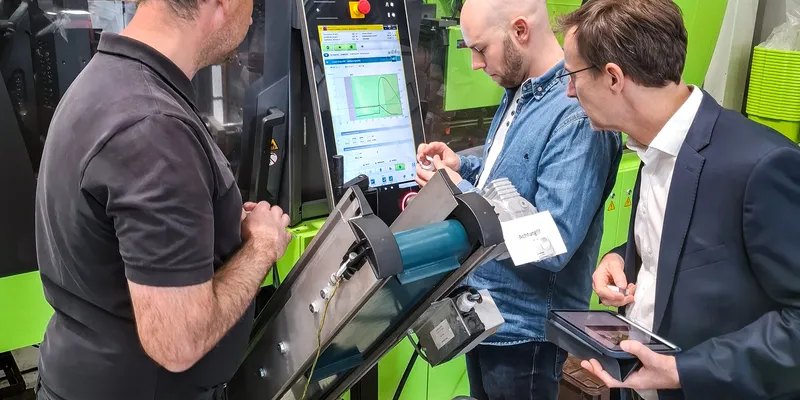
Using the software iQ weight control plus, the ENGEL victory 80 automatically adjusts the injection speed during injection molding in real time to match the current flow resistance. The system specifically leverages the physical characteristics of the process.
This results in an effect in the injection molding process that has received little attention to date but is nonetheless impressive: a significantly improved function of the non-return valve.
Real-time injection control with iQ weight control plus – How does it work?
At the start of the injection phase—during the decompression stroke—there is virtually no flow resistance. iQ weight control plus uses this window of opportunity to achieve maximum screw acceleration (up to approx. 80 cm³/s). This makes optimal use of the inertia of the shut-off ring: the non-return valve closes faster and more reliably.
As a result, the decompression stroke was reduced by 50%, giving Miraplast significantly more flexibility with the injection molding unit.
After this rapid initial phase, the system reduces the screw speed and fills the cavities gently and with controlled pressure.
What were the first visible results in terms of injection-molded part quality?
The results were fewer surface defects and cleaner molding of corners and ribs due to improved venting. This improvement in quality is already evident upon simple visual inspection.
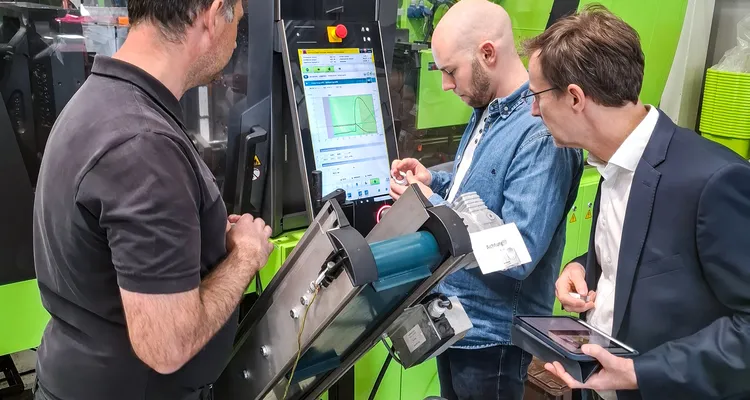
What measurable results has iQ weight control plus already achieved in the pilot production trial at Miraplast?
1) Improved part quality in injection molding—visible without measuring instruments
Reduced risk of surface defects
Cleaner molding of corners and ribs due to improved venting
Quality improvement already verifiable through visual inspection
2) Fast tooling approval—less reliance on skilled personnel
Only 2 adjustment parameters for tuning the injection motion: injection pressure + switch-over point
Production quality achieved after the 2nd iteration
High tolerance for insufficient balancing in multi-cavity molds
Pressure-controlled injection molding: A cavity failure does not immediately result in rejects in injection molding production
3) Sustainable process stability and energy efficiency
–10% energy consumption per cycle thanks to a smoother, pressure-optimized operating mode
Automatic compensation for gradual process fluctuations such as temperature, batch changes, or masterbatch thanks to integrated flow time control
Long running times without manual readjustment
4) More reliable non-return valve function
Faster and more reproducible closing of the non-return valve
Decompression stroke reduced by 50%
Greater flexibility and freedom of operation for the injection molding unit
The test results at Miraplast impressively demonstrate the potential of iQ weight control plus in real-world production, right from the very first use.
Read more about iQ weight control plus in an interview with development engineer Matthias Hüttler: How can iQ weight control plus reduce scrap in injection molding?.
We used iQ weight control plus in a pilot production run, and the results were impressive: stable processes, improved part quality, and a measurable reduction in energy consumption. This gives us a solid foundation for continued use.
Conclusion: With iQ weight control plus, reproducible part quality in injection molding is achieved, even with multi-cavity molds
iQ weight control plus delivers what technical injection molding production facilities need today: simpler sample testing that doesn’t require specialized personnel, consistent part quality, stable injection molding processes for multi-cavity molds, and measurable energy savings of –10% per cycle.
Miraplast was among the first to experience this potential in live production. The question for every production facility is not whether iQ weight control plus makes a difference, but when they will start to benefit from it.
Measurable results at a glance:
Decompression stroke reduced by 50% due to more reliable closing of the non-return valve
–10% energy consumption per injection molding cycle
Production-quality parts achieved after just 2 iterations
Automatic compensation for process fluctuations means fewer manual interventions
We’d be happy to show you what the system can do for your process.
FAQ
The gentle, pressure-controlled filling that follows the rapid initial acceleration reduces surface defects and improves venting in corners and ribs. The improvement in the quality of the injection-molded parts is already evident during visual inspection.
iQ weight control plus is particularly advantageous for multi-cavity molds, components with complex geometries, and in facilities seeking rapid mold validation with reduced reliance on skilled personnel.
With iQ weight control plus, debugging the injection motion requires only two injection molding process parameters: injection pressure and switchover time. At Miraplast, production-quality results were achieved as early as the second parameter iteration.
In addition, the system exhibits a high tolerance for insufficient balancing in multi-cavity molds. This significantly reduces setup effort and minimizes reliance on specialized personnel.
iQ weight control plus operates under pressure control during injection molding—which means that the injection speed is based on flow resistance. If no further volume flow is possible at the set pressure, the injection movement stops. This requires time-based switching, and here’s why: In the event of a cavity failure, a volume-based switching point would lead to an immediate process shutdown, since the defined volume would never be reached. Time-based switching, on the other hand, allows the system to continue the process stably even with a reduced number of cavities—without manual intervention and without scrap.
Thanks to its pressure-controlled, gentle operation with optimized injection pressure, iQ weight control plus reduces energy consumption per cycle by approximately 10%. At the same time, the integrated flow time control automatically compensates for gradual process fluctuations—such as temperature changes, batch changes, or masterbatch additions. As a result, the machine operates stably over long periods without requiring manual intervention.
iQ weight control plus regulates the injection speed during injection molding in real time based on flow resistance. At the start of the injection process—during the decompression stroke—the system uses the absence of counterforce to achieve maximum screw acceleration. This optimally utilizes the inertia of the locking ring, enabling the non-return valve to close faster and more reliably. At Miraplast, this allowed the decompression stroke in the injection molding process to be reduced by 50%.
-
digital solutions
-
technical molding

Related articles
-
![]() Optimizing production
 Eva WörnhörerSeptember 15, 2025How to Optimize your Injection Molding Process despite the Skilled Labor ShortagesSeptember 15, 2025Digital assistance systems help preserve machine expertise: This is how you can successfully optimize your injection mol ...
-
![]() Optimizing production
 Eva WörnhörerJanuary 24, 2024Increase OEE by 9% with production management softwareJanuary 24, 2024Since the introduction of authentig, the production management software at KROSCHU has networked 34 injection molding ma ...
-
![]() Optimizing production
 Eva WörnhörerJuly 1, 2025authentig production monitoring software: How SEZ DK is redefining production efficiencyJuly 1, 2025How can a machine park that has grown over time be made future-ready? SEZ DK shows how a modern production monitoring so ...
-
![]() Products & solutions
 Eva WörnhörerNovember 21, 2024Digitalization: a solution for skilled labor shortages & energy efficiencyNovember 21, 2024Digitalization provides the plastics industry with solutions for the shortage of skilled labor and energy efficiency. Di ...
-
![]() Optimizing production
 Eva WörnhörerMay 27, 2024Digital solutions: Proven in real-world applicationsMay 27, 2024Borgmann GmbH relies on digital solutions from ENGEL to maximize process stability and repeatability in production. The ...
-
![]() Products & solutions
 ENGEL TeamOctober 30, 2023Shopfloor monitoring & process monitoring at SolidPlastOctober 30, 2023SolidPlast from Poland specializes in the processing of polyoxymethylene (POM). The implementation of shopfloor monitori ...