- Home
- Blog
- Products & solutions
- How does Miraplast achieve consistent part quality in multi-cavity injection moulding, and why is the non-return valve crucial?
How does Miraplast achieve consistent part quality in multi-cavity injection moulding, and why is the non-return valve crucial?
In a pilot production trial using iQ weight control plus, Miraplast achieved fewer burnmarks, better quality in injection-moulded parts and significantly more reliable closure of the non-return valve. The result: production-quality parts after the second parameter iteration.

-
digital solutions
-
technical moulding
Miraplast Kunststoffverarbeitung GmbH – a company established over 60 years ago with sites in Würmla (Austria) and Hungary – is one of the first companies worldwide to use the latest product in the ENGEL inject AI portfolio in live production: iQ weight control plus.
The first deployment of iQ weight control plus on an ENGEL victory 80 demonstrated exactly what production professionals strive for:
significantly simplified trial runs
improved and reproducible injection-moulded part quality
optimal balancing for multi-cavity moulds
efficient injection moulding production despite a shortage of skilled workers
The results, expressed in figures, surprised even experienced set-up engineers:
Production-grade quality achieved after just the second parameter iteration – Simplified trial runs using just two injection moulding process parameters, even without specialist staff
10% reduction in energy consumption per cycle – thanks to pressure-optimised and material-friendly process control
50% reduction in the decompression stroke during the injection moulding process – thanks to a non-return valve that closes reliably and repeatably
Why is achieving consistent part quality in injection moulding with multi-cavity moulds such a challenge?
Consistently high injection-moulded part quality is crucial for the production of pipe clamp components using a 4-cavity mould. At the same time, process variations and the closing behaviour of the non-return valve make it difficult to achieve repeatable injection moulding production.
Typical challenges in day-to-day production:
Surface defects and venting problems at corners and ribs
Time-consuming sample testing requiring a high level of skilled labour
Gradual process fluctuations caused by temperature changes, batch changes or the addition of masterbatch lead to process instability
Unreliable closure of the non-return valve compromises the reproducibility of injection-moulded part quality
The key question was: How can process fluctuations be minimised, the closing behaviour of the non-return valve be stabilised and, at the same time, component quality ensured, without increasing set-up effort?
Miraplast Kunststoffverarbeitung GmbH employs around 80 staff at its main site in Würmla and operates 23 injection moulding machines, including 17 ENGEL machines. With a deliberately diversified product portfolio, the company cushions the impact of market fluctuations, for example in the automotive sector.
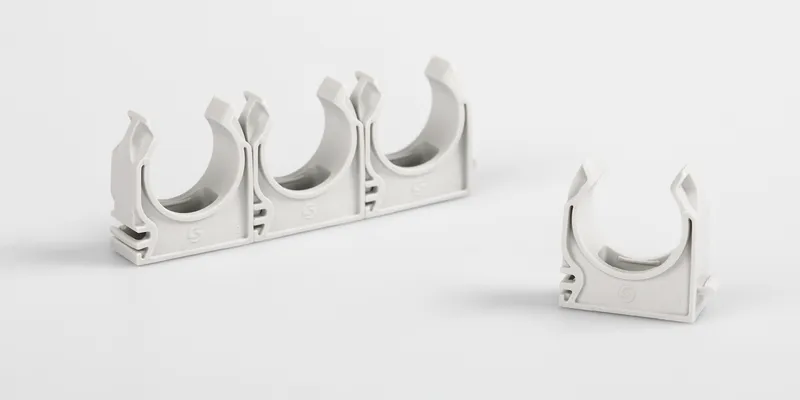
Pipe clamp components manufactured using a 4-cavity mould on an ENGEL victory 80
How did Miraplast manage to stabilise part quality in injection moulding, and what role does the non-return valve play?
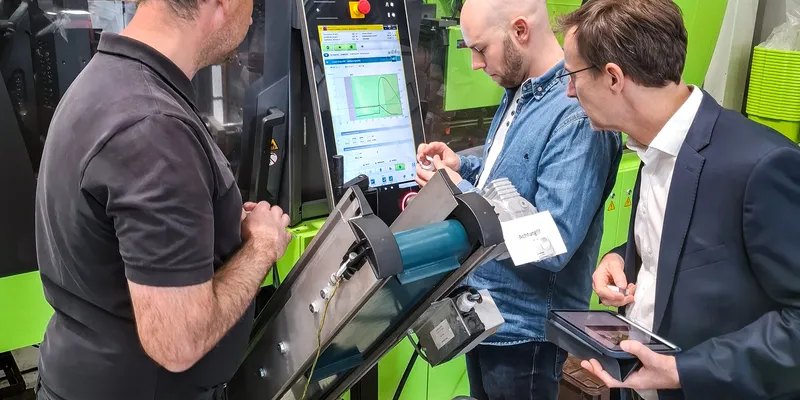
Using the iQ weight control plus software, the ENGEL victory 80 automatically adjusts the injection speed during injection moulding in real time to match the current flow resistance. The system makes targeted use of the physical characteristics of the process.
This results in an effect in the injection moulding process that has received little attention to date, yet is impressive: a significantly improved function of the non-return valve.
Real-time injection control with iQ weight control plus – How does it work?
At the start of the injection phase – during the decompression stroke – there is virtually no flow resistance. iQ weight control plus utilises this time window to achieve maximum screw acceleration (up to approx. 80 cm³/s). This makes optimum use of the inertia of the stop ring: the non-return valve closes more quickly and reliably.
As a result, the decompression stroke was reduced by 50 per cent, giving Miraplast significantly more flexibility with the injection moulding unit.
Following this rapid initial phase, the system reduces the screw speed and fills the cavities gently under pressure control.
What were the first visible results in terms of injection-moulded part quality?
The results were fewer surface defects and cleaner moulding of corners and ribs thanks to improved venting. An improvement in quality that is immediately apparent from a simple visual inspection.
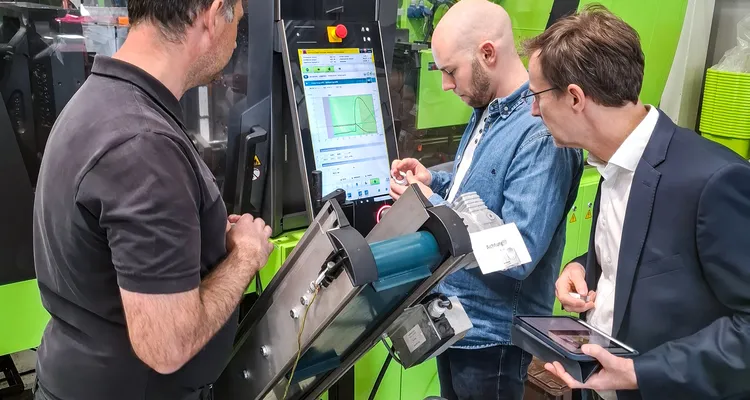
What measurable results has iQ weight control plus already achieved in the pilot production trial at Miraplast?
1) Improved part quality in injection moulding – visible without the need for measuring equipment
Reduced risk of surface defects
Cleaner moulding of corners and ribs thanks to improved venting
Improved quality already verifiable through visual inspection
2) Rapid trial moulding – less reliance on skilled personnel
Just 2 setting parameters for tuning the injection movement: injection pressure + switch-over point
Production quality achieved after the second iteration
High tolerance to insufficient balancing in multi-cavity moulds
Pressure-controlled injection moulding: a cavity failure does not immediately lead to rejects in injection moulding production
3) Sustainable process stability and energy efficiency
–10% energy consumption per cycle thanks to a smoother, pressure-optimised operating mode
Automatic compensation for gradual process fluctuations such as temperature, batch changes or masterbatch thanks to integrated flow time control
Long running times without manual readjustment
4) More reliable non-return valve function
Faster and reproducible closing of the non-return valve
Decompression stroke reduced by 50 per cent
Greater flexibility and scope for manoeuvre with the injection moulding unit
The test results at Miraplast impressively demonstrate the potential of iQ weight control plus in real production environments, right from the very first use.
Read more about iQ weight control plus in an interview with development engineer Matthias Hüttler: How does iQ weight control plus simplify injection moulding?.
We used iQ weight control plus in a pilot trial and the results were impressive: stable processes, improved part quality and a measurable reduction in energy consumption. This gives us a solid foundation for its continued use.
Conclusion: With iQ weight control plus, repeatable part quality in injection moulding is achieved, even with multi-cavity moulds
iQ weight control plus delivers what technical injection moulding production facilities need today: simpler sample testing that does not require specialist staff, consistent part quality, stable injection moulding processes for multi-cavity moulds and measurable energy savings of –10% per cycle.
Miraplast was among the first to experience this potential in live production. The question for every production facility is not whether iQ weight control plus makes a difference, but when they will start to benefit from it.
Measurable results at a glance:
Decompression stroke reduced by 50% thanks to more reliable closing of the non-return valve
–10% energy consumption per injection moulding cycle
Production-grade quality achieved during trial runs after just 2 iterations
Automatic compensation for process fluctuations means fewer manual interventions
We’d be happy to show you what the system can do for your process.
FAQ
The gentle, pressure-controlled filling following the rapid initial acceleration reduces surface defects and ensures better venting of corners and ribs. The improvement in the quality of the injection-moulded parts is already apparent on visual inspection.
iQ weight control plus is particularly beneficial for multi-cavity moulds, components with complex geometries, and in factories aiming for rapid trial moulding with reduced reliance on skilled labour.
With iQ weight control plus, trialling the injection movement now requires only two injection moulding process parameters: injection pressure and switchover time. At Miraplast, production-quality results were achieved after just the second parameter iteration.
Furthermore, the system exhibits a high tolerance to insufficient balancing in multi-cavity moulds. This significantly reduces set-up effort and minimises reliance on specialist staff.
iQ weight control plus operates under pressure control during injection moulding – this means that the injection speed is determined by the flow resistance. If no further flow rate is possible at the set pressure, the injection movement stops. This requires time-based switching, and here’s why: in the event of a cavity failure, a volume-based switching point would lead to an immediate process shutdown, as the defined volume would never be reached. Time-based switching, on the other hand, allows the system to continue the process stably even with a reduced number of cavities – without manual intervention and without rejects.
Thanks to its pressure-controlled, gentle operation with optimised injection pressure, iQ weight control plus reduces energy consumption per cycle by around 10 per cent. At the same time, the integrated flow time control automatically compensates for gradual process fluctuations – such as temperature changes, batch changes or masterbatch addition. As a result, the machine runs stably over long periods without requiring manual intervention.
iQ weight control plus regulates the injection speed during injection moulding in real time, depending on the flow resistance. At the start of the injection process – during the decompression stroke – the system utilises the absence of counterforce to achieve maximum screw acceleration. This makes optimum use of the mass inertia of the non-return ring, ensuring that the non-return valve closes more quickly and reliably. At Miraplast, this enabled the decompression stroke in the injection moulding process to be reduced by 50 per cent.
-
digital solutions
-
technical moulding

Related articles
-
![]() Products & solutions
 Eva WörnhörerNovember 21, 2024Digitalisation as the key to skills shortages and energy efficiencyNovember 21, 2024Digitalisation provides the plastics industry with solutions for the shortage of skilled workers and energy efficiency. ...
-
![]() Optimising production
 Eva WörnhörerMay 27, 2024Digital solutions: Practical success guaranteedMay 27, 2024Borgmann GmbH relies on digital solutions from ENGEL to maximise process stability and repeatability in production. The ...
-
![]() Products & solutions
 ENGEL TeamOctober 30, 2023Shopfloor monitoring & process monitoring at SolidPlastOctober 30, 2023SolidPlast from Poland specialises in the processing of polyoxymethylene (POM). The implementation of shopfloor monitori ...
-
![]() Products & solutions
 Eva WörnhörerFebruary 28, 2024Simply digitise: Paths to optimised plastics productionFebruary 28, 2024Plastics production is becoming increasingly digital, emphasises Zach in the interview. Digitalisation is particularly n ...
-
![]() Products & solutions
 Eva WörnhörerJuly 14, 2026How did Valrom reduce PVC scrap by 50% with iQ weight control?July 14, 2026Valrom shows how intelligent process control can tame even the most demanding materials in injection moulding. The resul ...
-
![]() Optimising production
 Eva WörnhörerSeptember 15, 2025How to produce injection moulded plastic parts without defects despite the skills shortageSeptember 15, 2025Digital assistance systems protect expertise at the machine: this is how you can successfully produce injection moulded ...